Steel connector sourcing becomes manageable when the drawing, material requirement, interface and acceptance records describe the same part. A familiar shape or certificate heading cannot resolve an unspecified thread, coating or batch. Buyers comparing manufacturers in China and other markets should establish that technical baseline before judging price, lead time or factory capacity.
Global buyers should source steel connectors from a controlled specification that states material, interface, thread or tube dimensions, coating, intended medium, and required records. ASTM A123/A123M and ASTM A153/A153M have different scopes for hot-dip zinc coatings, while ISO 4042 addresses electroplated coatings on threaded fasteners; none is a blanket approval for every connector. Compare suppliers on technical clarity and traceability before comparing unit price.
“「スチール製コネクタ」には、アダプター、圧縮式またはプッシュイン式のフィッティング本体、カップリング、ブラケット、および溶接・加工された接合部品が含まれます。調達における検討事項は、その部品が、定義された用途、インターフェース、市場規制、および発注書の証拠に適合しているかどうかです。.
Write the application as a measurable specification
信頼できる見積もり依頼は、接続部の機能(チューブの結合、ねじの変換、エア配管の引き回し、または部品の固定)から始まります。管理図面、関連する場合はチューブの外径、ねじの呼び、シール方法、材質、表面処理、数量、および梱包要件を含めてください。ねじのファミリー、ピッチ、テーパー、およびシール方式が異なる場合があるため、「1/4インチねじ」という表記だけでは不完全です。.
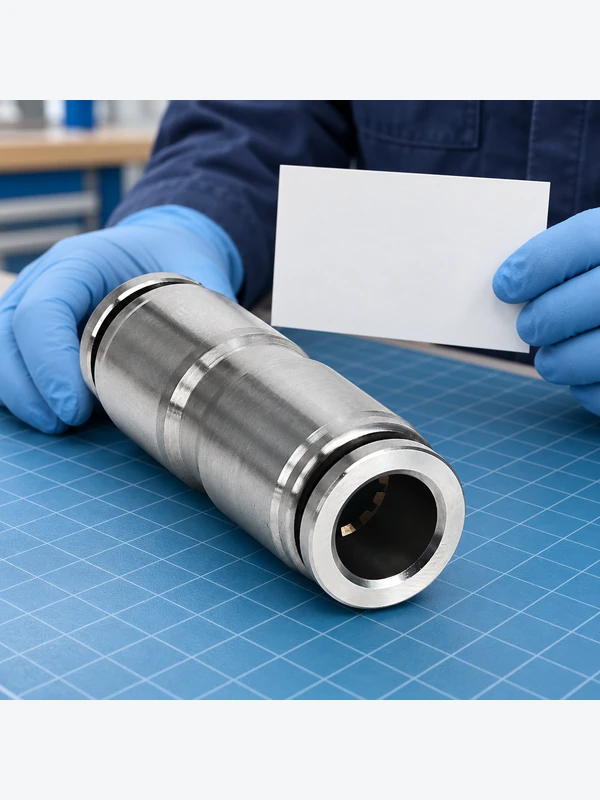
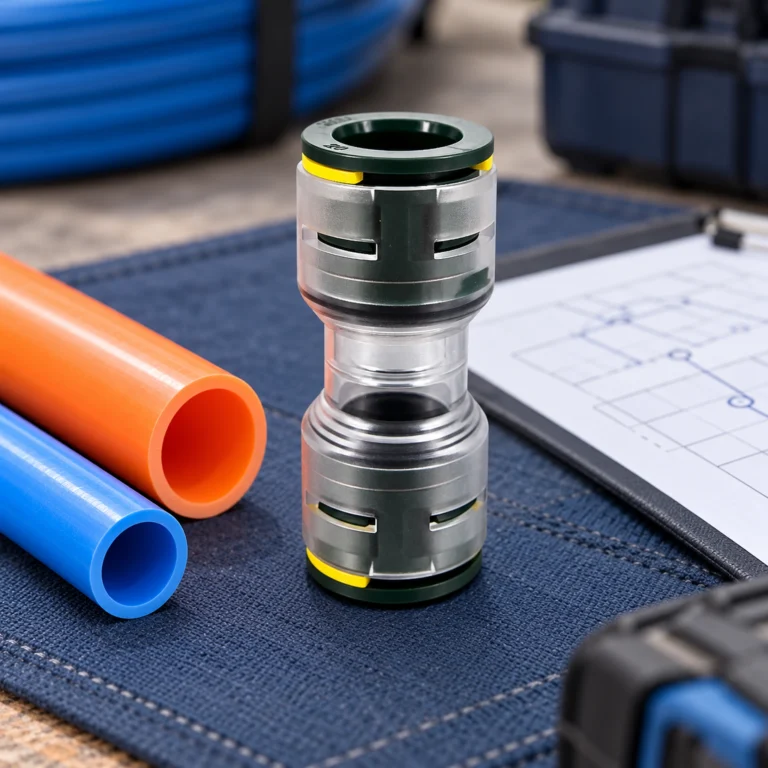
媒体、温度範囲、設置環境、プロジェクトの制約事項を記載します。シリーズを比較している購入者にとって、このワンタッチ継手の概要は、プッシュイン式インターフェースと、ねじ込み式または圧縮式の接続を区別するものです。.
| 仕様フィールド | 記載すべきこと | なぜそれが調達に影響するのか |
|---|---|---|
| 接続インターフェイス | チューブ外径、ねじの呼び、嵌合部品、シール種類 | 公称寸法の前提や仮組みに関するトラブルを防ぎます |
| 素材と仕上げ | 要求される鋼種またはステンレス鋼種、塗装システム、必要に応じた色またはマーキング | サプライヤーが代替品や加工制限を特定できるようにする |
| 利用規約 | 媒体、温度、露出、設置場所 | 汎用的なカタログの謳い文句ではなく、その部品が持つ本来の用途に結びつけています |
| 受領証拠 | Drawing revision, inspection plan, lot identification, agreed records | 受入検査と不適合処理を実用的なものにする |
Use each standard only for its stated scope
すべての規格番号について、現在の適用範囲および正確な製品と照らし合わせて確認してください。ASTM A123/A123Mは組立鉄鋼製品の溶融亜鉛めっきを対象とし、ASTM A153/A153Mはハードウェアを対象としています。また、ISO 1461も組立品を対象としています。これらの文書は、特定の接続金具が特定の圧力、荷重、化学物質、または市場の要件に適合することを証明するものではありません。.
ISO 4042 addresses electroplated coating systems for threaded components, while EN 10204 classifies metallic-product inspection documents. The contract must still define the needed document type and traceability. Treat a cited standard according to its scope—not as a product certification claim.
赴任国の規則により、ラベリング、安全要件、または税関の要件が追加される場合があります。輸入者、プロジェクトオーナー、および責任ある技術部門は、コンプライアンスに関する表明を行う前に、適用されるルートを確認する必要があります。.
Read what a 3.1 certificate actually covers
An EN 10204 type 3.1 document is an inspection document, not a blanket approval for a connector assembly. Holland Applied Technologies explains the distinction between 3.1 and 3.2 documents: type 3.1 includes specific inspection results validated by the manufacturer’s authorized inspection representative independent of manufacturing. Type 3.2 adds the relevant independent validation arrangements. The contract must define which document is required and for which supplied product.
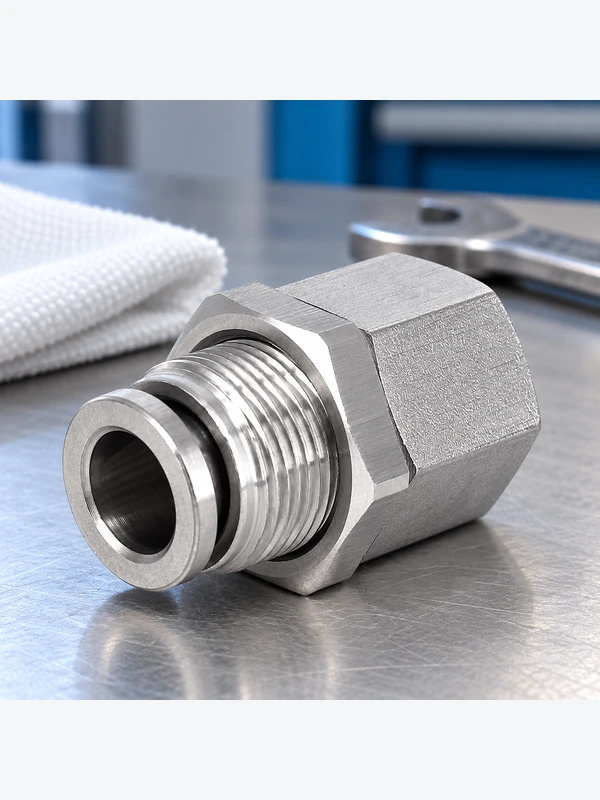
Do not reduce this to a request for a certificate with a recognizable logo. Check the producer, product description, material specification, order reference, heat or batch identification and the reported results. The shipped goods must be traceable to the document. A valid record for an upstream material does not, by itself, establish that the finished connector’s dimensions, seals, coating and assembled performance satisfy the purchase order.
Separate the evidence into three questions: is the specified material documented; is the finished component dimensionally correct; and does the assembled connection meet its service and acceptance requirements? The steel pipe coupling specification guide can help organize the last two questions. Request only documents that answer an actual requirement, and identify any missing evidence before dispatch rather than during site installation.
Check the factory beyond the first sample
サンプルで形状や仕上がりを確認することはできますが、量産供給は別の能力の問題です。メーカーがどのように改訂版を管理し、ロッドを特定し、材料を管理し、不適合品に対処しているかについて尋ねてください。提出された仕様に適合するものと代替されるものの明確な明示を求めてください。.
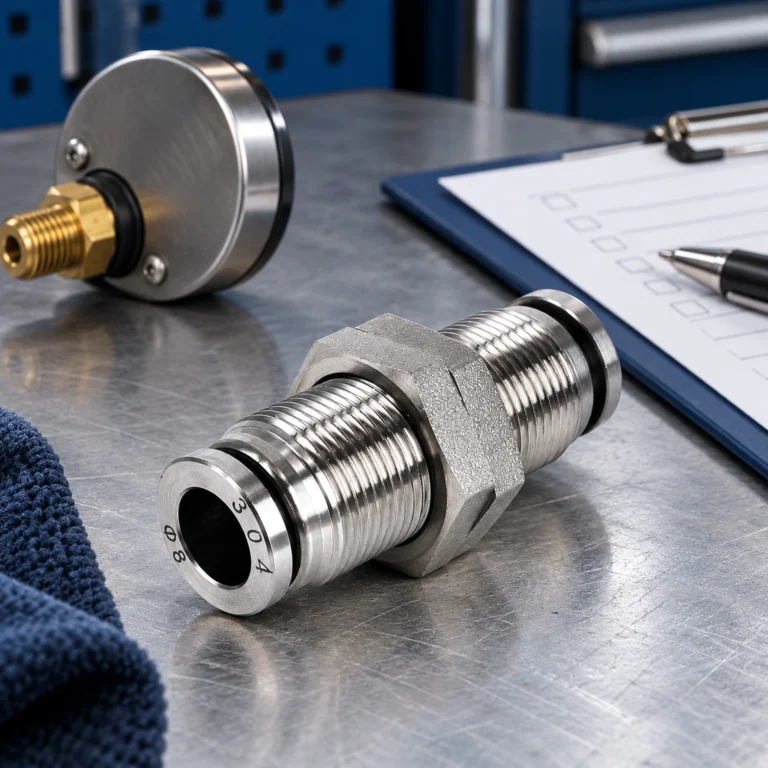
For sourcing in China or elsewhere, compare the production and communication system rather than national labels. Review technical annexes, dimensional tolerances where applicable, tooling or sample status, packing, and change notification. A factory visit or independent inspection may suit a higher-risk order when its scope is agreed in advance. Keep pneumatic and structural connection categories separate; this primer on stainless-steel joints helps organize application-specific enquiries.
| 比較点 | サプライヤーへの質問 | 商業効果 |
|---|---|---|
| テクニカルマッチ | 見積書には、図面、インターフェース、材料、仕上げについて記載されていますか? | 異なる項目の比較リスクを軽減します |
| 文書管理 | 改訂、ロットラベル、および承認された変更はどのように管理されていますか? | 小切手の受領と是正処置をサポートします |
| 検査支援 | 注文書には、どのような合意済みの測定値または記録を添付できますか? | 出荷前に現実的な受領基準を設定する |
| 梱包と物流 | サイズはどのように区別され、保護され、ラベル付けされ、発送されますか? | 仕分け、破損、および設置の遅延を削減できます |
| 総コスト視点 | 除外事項、最小数量、治工具、運送条件、およびリードタイムの前提条件は何ですか? | 低単価が下流工程のコストを不明瞭にするのを防ぎます |
Define how an approved sample becomes a repeatable order
A sample is useful only when its identity can be carried into production. Record the part number, drawing revision, measured interfaces, material and finish, supplied seals, packing arrangement and any deviations accepted during the trial. Keep the approved sample or its controlled inspection record available to both the supplier and receiving team. A photograph of a good-looking part is an incomplete reference for a later shipment.
Ask the supplier to state which changes require approval. A change in steel grade, coating process, machining source or seal material can affect a previously accepted configuration even when the catalogue name remains unchanged. The purchase order should name the notification route and the records needed to assess a proposed substitution. This is a recommended purchasing control, not evidence that any particular manufacturer already operates such a system.
For pneumatic components, compare the hose-and-fitting manufacturer qualification checklist with the connector enquiry. Both benefit from a traceable sample and a clear mating interface, but their test conditions and acceptance criteria may differ. Define what the receiving team can check without destructive testing and which records must come from the supplier or an agreed laboratory.
Handle deviations explicitly: identify the affected lot, quarantine suspect parts where appropriate, record the nonconformity and agree the disposition before use. Avoid silently accepting an alternative because installation is waiting. A controlled concession should specify its scope and approval; it should not automatically amend every future order.
Compare quotations with inspection and delivery risk
有用な引用文は、その照会まで遡って確認することができます。アイテムコード、リビジョン、数量、材質、仕上げ、寸法、インコタームズ、金型、梱包、記録、リードタイム、および除外事項を比較してください。「同等」の材質またはコーティングが提案された場合は、出荷前に正確な代替品と技術的な承認を求めてください。.
総コストには、陸揚げ価格以上のものが含まれます。例えば、現場での仕分け、緊急の代替輸送、据え付けの一時停止などは、わずかな単価の差を上回ることがあります。書類作成は、コネクタの役割とミスのコストに見合ったものにしてください。.
商品の到着前に受け入れ検査の設定を行います:荷物の身元と数量を確認し、マーキングと寸法を承認された書類と比較し、損傷を記録し、不一致品を隔離します。空気圧ラインプロジェクトに関して、このエアストレート継手のガイドは、配管の要件と材料およびインターフェースの要件を区別しています。.
Follow the same checks for every supplier
- 管理されたテクニカルパッケージを発行し、サプライヤーに対して前提条件、例外事項、および代替案の提示を求めてください。.
- 商業条件の前に技術的な適合性を比較せよ。無条件の安さよりも、完全な提案の方が役立つ。.
- 発注書において、必要な記録、ラベル、包装、および検査項目について合意する。.
- 出荷先市場の責任を確認し、裏付けのない性能または認証に関する表現を避けてください。.
OULUは製品オプションや問い合わせ情報の整理を支援しますが、最終的な選定は購入者の確認済み仕様および技術レビューに依存します。.
Keep the drawing, standard, and batch together
Global sourcing becomes difficult when the drawing uses one designation, the quotation uses another, and the inspection report omits the coating or heat number. Create one controlled package containing the approved drawing, material and coating requirement, applicable standard edition, inspection points, packing instructions and change-notification rule. Ask the supplier to identify what is tested on every batch and what is checked only during qualification.
| File | Minimum information | Buyer check |
|---|---|---|
| Drawing | Dimensions, tolerances, holes, threads and finish | Matches the installed interface |
| Material record | Grade, heat or batch reference and coating | Traceable to the shipped lot |
| Inspection plan | Critical dimensions, sampling and acceptance limits | Can be used at receiving |
| Change control | Approval route for material, tooling or process changes | Prevents silent substitutions |
Compare this process with the construction steel connector checklist そして request a drawing review before placing a global order.
よくある質問
鋼製コネクタの購入者が考慮すべき基準は何ですか?
Consider Standards that match the component and question: coating scope, fastener properties, inspection documentation, or finished-assembly requirements. ASTM A123/A123M, ASTM A153/A153M, ISO 1461, ISO 4042, and EN 10204 can be relevant. Confirm current editions, scope, and contractual applicability before ordering.
鋼製コネクターのメーカーをどのように評価すればよいですか?
サプライヤーが図面通りに製造する能力、材料および仕上げの特定、改訂管理、部品の梱包、および合意された記録を提供する能力を評価してください。例外や不適合部品がどのように伝達されるかを確認します。サンプル単体では、継続的な発注管理を裏付けることはできません。.
サプライヤーはどのような材質とコーティングの情報を提供すべきですか?
材質の説明またはグレード、コーティングの種類、必要に応じて適用規格、および制限事項や代替品について確認してください。情報を文脈の中で検討できるように、使用環境と嵌合材料を定義してください。「スチール」や「亜鉛めっき」だけでは完全な説明ではありません。.
鋼製コネクターの見積もりを比較するにはどうすればよいですか?
技術的コンテンツ(インターフェース、寸法、材質、仕上げ、リビジョン、数量、記録、梱包、除外事項)を最初に標準化します。次に、インコタームズ、金型、リードタイム、および支払条件を比較します。これにより、価格差が単に魅力的であるだけでなく、説明可能なものになります。.
注文にはどのような検査記録を添付すべきですか?
リスクレベルに応じて必要とされる国家(州)の記録:パッキングリスト、ロット識別、寸法検査、材料明細書、または合意された検査文書。EN 10204は有用な用語ですが、契約に必要なものを決定するものではありません。生産の前に、受入計画と記録をすり合わせてください。.
1つの鋼製コネクタの仕様で、あらゆるグローバル市場に対応できるでしょうか?
通常、レビューなしでは成り立ちません。アセンブリ、ローカルルール、顧客ドキュメント、環境曝露、および輸入責任は市場によって異なる場合があります。コア仕様を構築してから、同等性やコンプライアンスを主張する前に市場固有の要件を確認してください。.
What is the practical difference between EN 10204 type 3.1 and 3.2?
Type 3.1 uses the manufacturer’s authorized inspection representative independent of manufacturing to validate specific inspection results. Type 3.2 includes additional independent validation under the applicable arrangements. Specify the document type, product and traceability requirements in the contract rather than treating either number as an assembly certification.
Does a material certificate replace a finished connector inspection?
No. Material evidence and finished-component acceptance answer different questions. Verify drawing dimensions, threads, seals, finish and any agreed functional tests separately, while maintaining the traceability needed to connect the supplied lot to its documents.
参考文献
- ASTM A123/A123M:鉄鋼製品の亜鉛めっき(溶融亜鉛めっき)コート
- ASTM A153/A153M:鉄鋼製ハードウェアの亜鉛めっき(溶融亜鉛めっき)
- ISO 1461:鉄鋼製加工品の溶融亜鉛めっき被膜
- ISO 4042:締結用部品-電めっき層
- EN 10204: 金属製品—検査文書の種類
- Holland Applied Technologies: Difference Between EN 10204 3.1 and 3.2 Inspection Certificates
Summary
A reliable steel connector order links the drawing, interface, material, finish and inspection evidence to the shipped lot. Use each standard for its stated scope, and check what a 3.1 or 3.2 document covers before relying on it. Approve the complete sample configuration, control substitutions and agree receiving checks in advance. These steps make quotations comparable and give both parties a clear way to resolve a discrepancy.