Buying pneumatic hose and fittings from a China manufacturer requires a defined assembly, not just a tube size and a catalogue photograph. For ANMASPC or any alternative supplier, the useful questions concern actual dimensions, permitted operating conditions, mating interfaces and evidence for the supplied configuration. This guide turns those questions into a sample-approval and repeat-order process.
For China sourcing, specify hose or tube material, outside and inside diameter, working-pressure range, temperature, media, end connection, and test evidence before comparing quotations. One bar equals 100 kPa, but a pressure number alone does not establish a safe assembly; ISO 4414 is a system-safety standard, not a supplier certification. The practical action is to issue a controlled requirement sheet, obtain matched hose-and-fitting samples, and verify fit, leakage, and documentation under the intended duty cycle.
Pneumatic hose and fittings move air between preparation units, valves, actuators, and tools. A nominally correct tube can still leak, kink, abrade, or release when its cut, tolerance, fitting, seal, or environment is uncontrolled.
Specify the hose and fitting together
Start with material and operating environment.
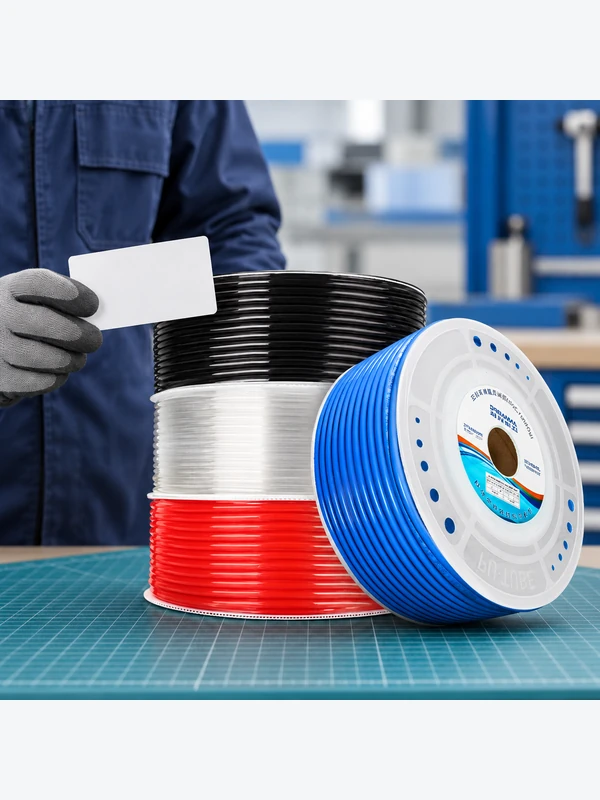
Polyurethane (PU), polyamide (PA/nylon), rubber, and PVC trade flexibility, abrasion resistance, temperature behavior, chemical compatibility, and routing. Identify air quality, oil or cleaning-agent exposure, UV, bend radius, vibration, and nearby heat. Confirm material against the supplier’s data sheet and actual media; “air hose” is not a compatibility study.
Separate working pressure from burst pressure.
Request a working-pressure range at installation temperature, plus the test method and sample condition. Pressure changes with temperature and construction; a burst result is not a permitted operating pressure. ISO 4414:2010 covers foreseeable misuse, stored energy, isolation, and maintenance. For US workplace cleaning, OSHA 29 CFR 1910.242(b) requires compressed air to be reduced to less than 30 psi and used only with effective chip guarding and personal protective equipment. This cleaning rule is not a working-pressure limit for machine tubing.
Control dimensions, threads, and assembly method.
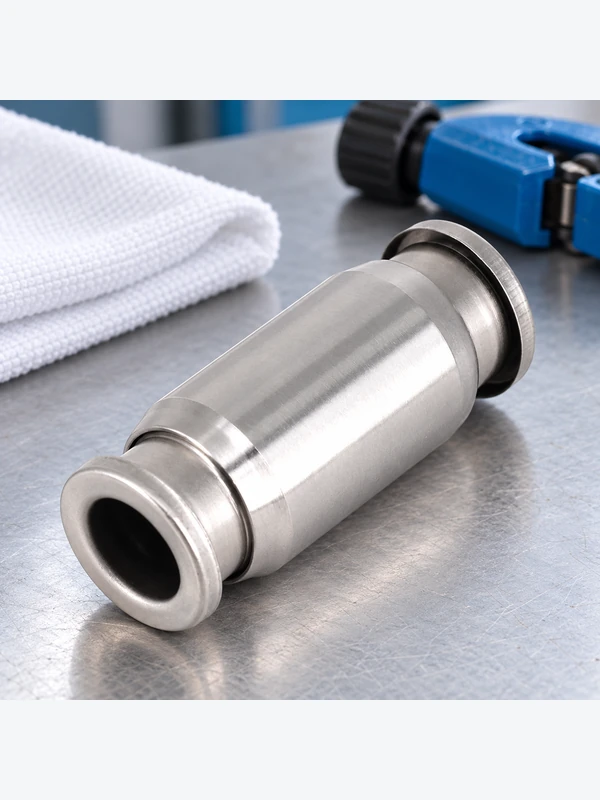
For push-to-connect systems, tube outside diameter is usually the critical interface; inside diameter influences flow and pressure drop. Confirm metric versus inch sizes, tolerance, ovality limits where relevant, minimum insertion depth, and whether field cuts must be square and burr-free. For threaded fittings, specify thread family and sealing method—such as BSPP, BSPT, NPT, or metric—rather than assuming that a similar nominal size will mate safely. This is also a useful point to distinguish pneumatic tubing from microduct connectors, which serve different network and sealing applications.
Identify the thread and seal on both sides of the fitting
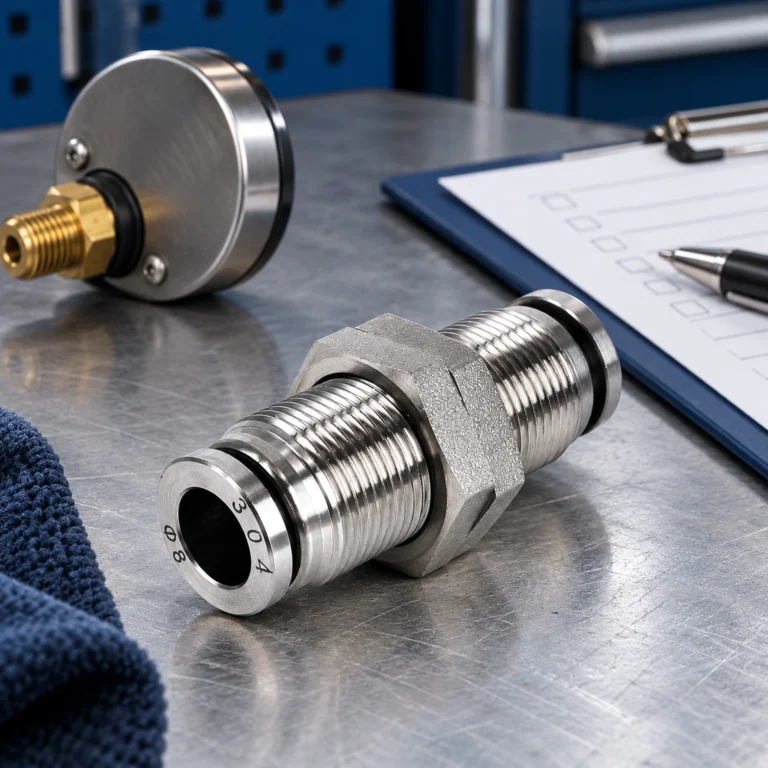
Identification des fils should be part of sample approval. A supplier’s description such as quarter-inch male does not establish BSPP, BSPT, NPT or a metric interface. The Hosemaster’s thread comparison explains that BSP and NPT have different flank angles. Nominal size and partial hand engagement therefore cannot establish a compatible pressure connection.
Request a drawing that names the thread at the component port and at the fitting, together with the specified sealing arrangement. Parallel-thread fittings may use a defined face seal or washer; tapered connections use their documented mating geometry and assembly practice. Do not assume that adding sealant makes a mismatched thread acceptable. If a transition is needed, specify an adapter whose two ends and service limits are known.
Use the pneumatic thread-matching guide when preparing the enquiry. During the sample trial, also check tool access, tubing insertion and the space needed to release or replace the fitting. An interface that can be assembled on a bench may still be awkward to service inside a machine guard. Record the actual mating part, not merely the supplier’s family name.
Compare the complete delivered assembly
| Procurement dimension | Lowest-price quote | Specification-led quote | Que vérifier |
|---|---|---|---|
| Compatibility | May list only nominal size | States tube OD/ID, thread, seal, and mating part | Assembly drawing and physical fit |
| Performance evidence | General claim | Links range, temperature, and test method | Leak and pressure test record for sample |
| Durability risk | Material may be unspecified | Material and environment limits identified | Data sheet; bend and abrasion needs |
| Maintenance and returns | Higher inspection burden | Traceable lots and replacement terms defined | Lot marking and nonconformance process |
| Total cost tendency | Lower initial cost | Lower uncertainty; not automatically lower cost | Illustrative rework, downtime, and freight exposure |
An illustrative total-cost review includes part cost, incoming checks, rejected assemblies, replacement freight, installation labor, and downtime exposure. Do not count a test claim as a saving until the configuration is verified.
Put the operating details in the purchase request
Send one controlled checklist to every bidder, then compare exceptions line by line. For related valve, regulator, and accessory context, see the site’s pneumatic parts; the bill of materials should still identify the exact mating components.
| Requirement | Specification to record | Preuve d'acceptation |
|---|---|---|
| Application and media | Machine, air quality, oil/chemical contact, indoor/outdoor use | Supplier compatibility statement and data sheet |
| Hose/tube geometry | Material, OD, ID, wall, length, bend-radius need, colour | Dimensional inspection plan; sample measurement |
| Enveloppe opérationnelle | Normal and maximum pressure; temperature; duty cycle | Published range with named test basis |
| Fitting interface | Push-in, barb, or thread type; thread standard; seal | Mating drawing and assembly trial |
| Quality and logistics | Lot ID, packaging, inspection level, delivery terms | Sample report, packing specification, agreed records |
Check the rules for the destination market
Standards frame questions; they do not transfer automatically from a data sheet to a finished assembly. ISO 4414:2010 covers general safety requirements for pneumatic fluid-power systems, not manufacturer certification. ISO 12100 provides a machinery risk-assessment framework, while ISO 8573-1 classifies compressed-air contaminants. In the EU, applicability of Directive 2014/68/EU depends on the assembly’s design, fluid, pressure, volume, market, and exclusions—seek qualified review rather than assuming a mark is required.
Ask what each document covers: material declaration, inspection report, test method, product declaration, or third-party certificate. Unsupported claims can create tender, safety, warranty, and liability exposure. Near telecom duct routes, HDPE microducts remain a separate system, not a pneumatic-hose substitute.
Approve the manufacturer with samples and records
- Issue the same technical checklist, drawing, quantity, and destination-market requirements to each supplier.
- Request a sample assembly representing the exact tube, fitting, thread, seal, and packaging configuration to be ordered.
- Inspect dimensions and workmanship, then conduct an agreed leak or pressure test using a documented method suitable for the application.
- Review lot identification, change-control practice, lead-time assumptions, and the process for nonconforming goods before approving a production order.
When evaluating ANMASPC alongside other China manufacturers, use the same evidence-led scorecard; ask for configuration-specific documentation and sample support rather than inferring capabilities from a brand name. That approach makes sourcing discussions more comparable and protects engineering change control.
Keep repeat shipments tied to the approved configuration
After a sample passes the agreed checks, turn its identity into a purchasing record. Record the tube material, size and tolerance basis, fitting code, seal, thread, drawing revision, colour where relevant, packaging and lot identification. Attach the test method and results that supported approval. A sample is a reference configuration; it is not proof that every later batch will be identical without inspection and change control.
Ask which production changes trigger notification. Resin formulation, wall construction, fitting seal or component source changes may require engineering review even when the outward appearance remains similar. State who can approve an alternative and which measurements or tests are required before release. Keep this proportionate to the application instead of requesting unrelated automotive or medical certifications for an ordinary pneumatic assembly.
The comparison of PU and PA air hose is useful when material is still undecided, but the selected supplier’s exact data remains necessary. Establish pressure at the intended temperature, route bend requirements, media exposure and compatible fittings for the chosen construction. A material name alone cannot answer those questions.
At receipt, compare package labels and lot references with the order, inspect the agreed dimensions and workmanship, and retain the required records. If a leak or pull-out occurs, capture the tube cut, measured diameter, fitting identity, insertion condition and operating circumstances before replacing parts. This creates a useful investigation trail without assuming either installation error or a manufacturing defect in advance.
Ask for a complete hose assembly sample
A hose manufacturer may quote tubing, couplings, clamps and packaging separately. The field failure usually occurs at the interface between them, so ask for a sample assembled with the intended hose ID, coupling profile, seal and retention method. Test the sample under the project’s pressure, temperature and movement conditions before approving a repeat order.
| Sample check | Que faut-il enregistrer | Why it matters |
|---|---|---|
| Hose construction | Layers, material, ID, OD and bend requirement | Confirms the quoted hose matches the duty |
| Coupling fit | Profile, thread, seal and retention method | Prevents leaks and unsafe substitutions |
| Pressure evidence | Working versus burst rating, test medium and temperature | Stops a burst number being used as a working limit |
| Batch control | Part number, production lot and inspection record | Supports receiving and later investigation |
For welding-area use, compare the hose safety guide; for fitting families, see the air hose fitting comparison.
Foire aux questions
What should I look for in a pneumatic air hose manufacturer in China?
Look for clear configuration data, responsive technical clarification, representative samples, traceability practices, and documentation that distinguishes tested facts from marketing language. Compare suppliers against one written requirement sheet, then record any exceptions before purchase approval.
Which hose material is best for compressed air?
There is no universal best material. Select PU, PA, rubber, PVC, or another construction based on pressure, temperature, flexibility, abrasion, media, and installation conditions; confirm the proposed material against the supplier’s data for the intended service.
How do I verify hose and fitting compatibility?
Match the tube’s actual outside diameter and tolerance to the fitting specification, and confirm the fitting’s thread and sealing arrangement with its mating part. Use a representative assembly trial with square, burr-free cuts, then retain the approved configuration as the purchasing reference.
What documents should a pneumatic hose supplier provide?
Request a data sheet, dimensional specification, material information where relevant, configuration drawing, packaging and lot-identification details, and any agreed inspection or test record. For destination-specific compliance, ask what the document covers and who issued it; do not assume every report is a certification.
Can a pneumatic hose be used near welding or hot work?
Only after a documented risk assessment confirms the hose material, temperature rating, routing, and protection are suitable. Welding sparks, radiant heat, and damage from traffic can change the risk quickly, so isolate air where needed and follow site hot-work controls.
How should I qualify a China manufacturer before placing a bulk order?
Begin with a controlled specification and sample, verify fit and agreed test evidence, and review traceability, change notification, packaging, and corrective-action handling. A first order can include defined inspection points and acceptance criteria so that commercial scale follows demonstrated conformity.
Can BSP and NPT pneumatic fittings be substituted if they screw together?
No. Partial engagement does not prove matching thread geometry or a proper sealing interface. Identify both ends and use the documented mating components or a correctly specified adapter. Do not compensate for a mismatch with extra torque or sealant.
What should change between sample approval and a bulk purchase order?
The accepted sample should become a controlled configuration with a part number, drawing revision, materials, mating interfaces, acceptance checks and lot records. Define the approval route for changes and apply the agreed receiving checks to repeat shipments.
Références
- ISO 4414:2010 — Transmissions pneumatiques : règles générales et exigences de sécurité
- ISO 12100:2010 — Safety of machinery: risk assessment and risk reduction
- ISO 8573-1:2010 — Compressed air contaminant classes
- OSHA 29 CFR 1910.242 — Outils et équipements à main et portatifs à moteur
- Directive 2014/68/EU — Pressure equipment
- The Hosemaster: BSP vs NPT—What’s the Difference and Are They Compatible?
Résumé
Qualify a pneumatic hose manufacturer against the complete assembly you intend to install. Confirm tube dimensions and operating limits, identify both thread and sealing interfaces, and approve a representative sample using agreed checks. Carry that configuration into the purchase order with traceable lot records and change notification. This provides a practical basis for comparing ANMASPC and other suppliers without turning catalogue descriptions or an isolated test result into unsupported performance claims.