When a process engineer in Oulu traced inconsistent pick-and-place motion at an injection-molding cell, she first changed a valve setting. The gripper still hesitated, and a hiss appeared at full reach. The root cause was not a failed valve: the tube-to-elbow connection had not allowed for movement, tube material, or the fitting’s flow path. Re-specifying the interface and verifying the branch addressed the problem.
クイック回答: pneumatic fittings in plastic manufacturing connect air preparation, valves, cylinders, grippers, and blow-off points; select them for the complete duty, not nominal thread size alone. ISO 6358-1 expresses pneumatic-component flow characteristics, while ISO 8573-1 classifies compressed-air contaminants. Record tube outside diameter, port thread, media, limits, motion, and exposure; then test the completed assembly for leakage and function before release.
Related reading: air-hose fitting comparison.
Where pneumatic fittings are used in plastics processing
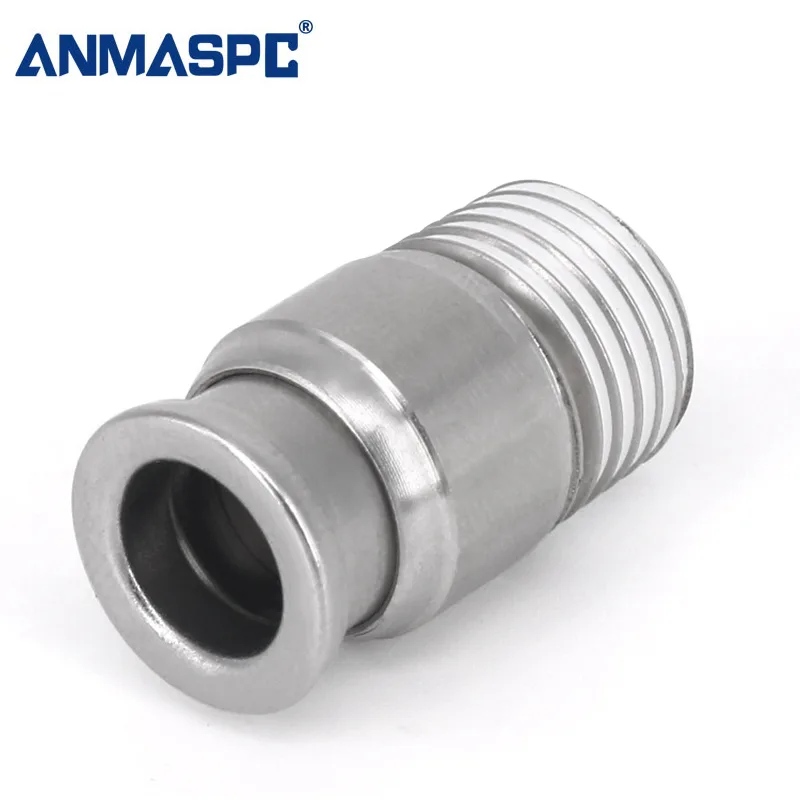
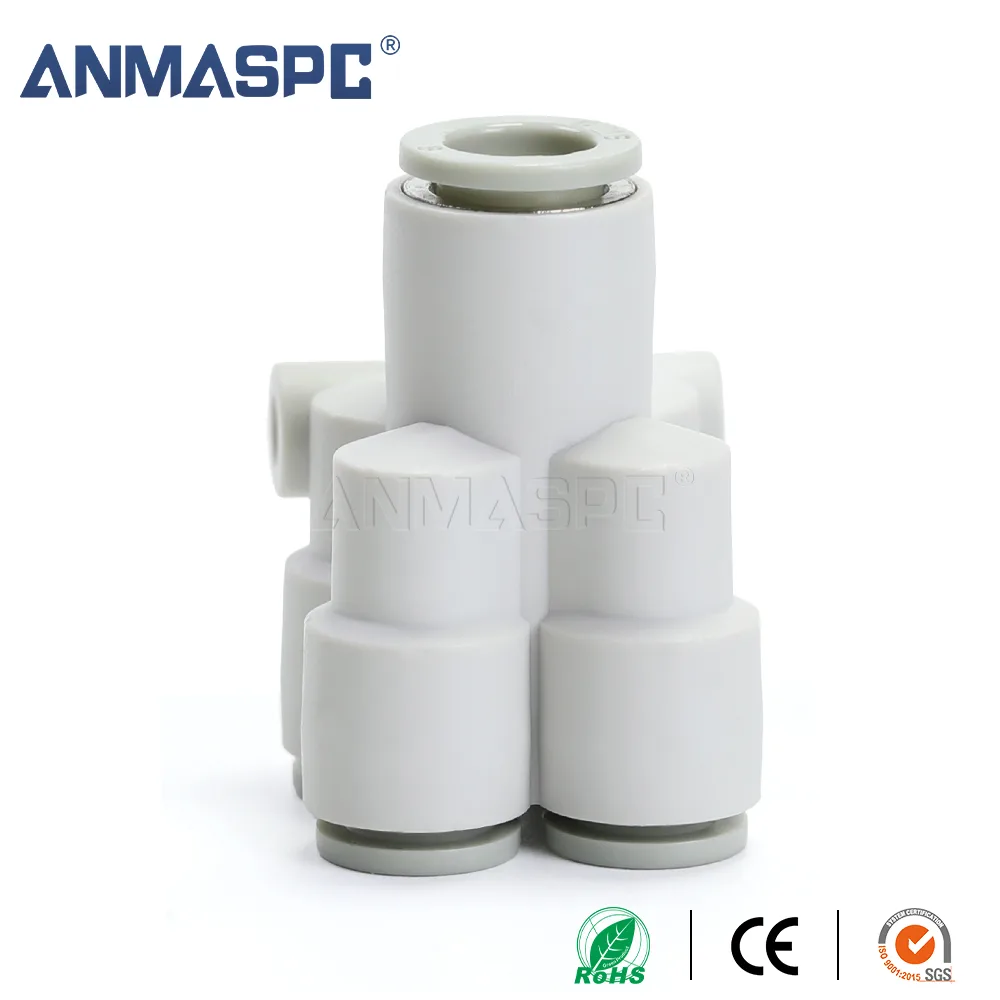
圧縮空気 operates actuator control, robotic end effectors, conveying auxiliaries, valve islands, part ejection, and controlled blow-off. Fittings make these circuits serviceable: straight connectors extend a route, elbows manage direction changes, tees feed branches, and threaded adapters connect equipment ports. Each fitting is both a connection and part of the flow path.
For a molding-cell or extrusion-line buyer, ask whether the entire branch can supply the intended motion. ISO 6358-1 is a test method for flow-rate characteristics of pneumatic components with compressible fluids; it supports comparable data instead of an unqualified “high-flow” description. Include tube internal diameter and length, reducers, valve-port size, and actuator demand in the review.
| Plastics-manufacturing duty | Typical fitting role | Selection priority | Installation check |
|---|---|---|---|
| Robot gripper or pick-and-place arm | Elbow or swivel-oriented tube connection | Tube flexing, clearance, side-load control, and flow path | Observe a full representative motion cycle |
| Mold ejector or pneumatic cylinder | Threaded port adapter or straight fitting | Correct thread form, seal method, and branch capacity | Leak-test at the documented operating condition |
| Conveying or air-assist auxiliary | Tee, reducer, or manifold connection | Shared branch demand and accessible isolation | Check pressure change when adjacent users cycle |
| Part cooling or approved blow-off point | Tube-to-port connection | Purpose, guarding, and applicable site safety controls | Verify the nozzle and air-use practice separately |
Match the fitting, tube, and air quality to the process
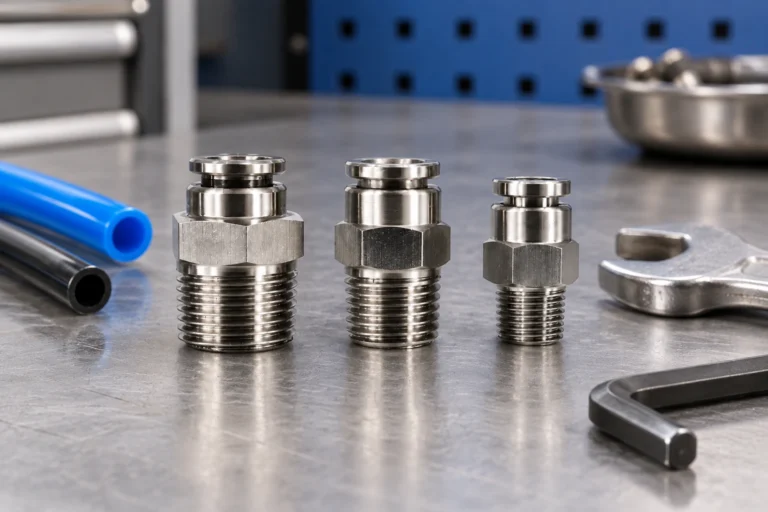
A fitting body alone does not define compatibility. Engineered-polymer, brass, and stainless-steel constructions have different considerations, while the seal and tube may be limiting components. Start with the compressed-air condition, lubricant carryover, moisture, cleaning agent, heat, and contact time. Ask for model-specific material and seal guidance rather than inferring chemical resistance from a generic material name.
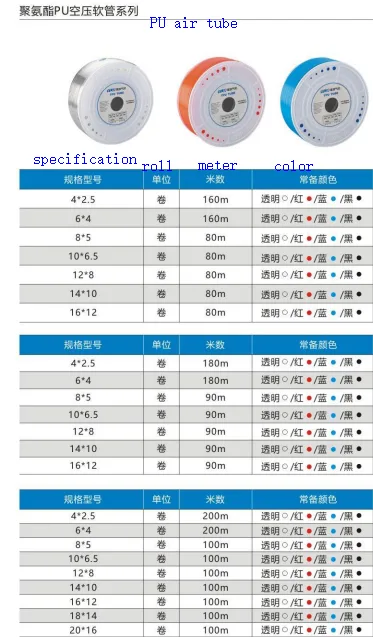
Tube selection matters equally at a push-in connection. Polyurethane tubing can offer routing flexibility, whereas polyamide tubing provides a different stiffness balance. Buyers comparing PU and PA air hose should confirm the approved tube range, outside-diameter tolerance, bend radius, and installation condition. ISO 8573-1 classifies particles, water, and oil in compressed air; it is not a fitting-material certificate.
| Condition to document | Information required from the application | 調達への影響 |
|---|---|---|
| チューブインターフェース | Tube OD, material, hardness, bend radius, and movement | Confirms gripping, sealing, and routing suitability |
| ポートインターフェース | Thread designation, size, gender, and sealing geometry | Avoids joining similar-looking but incompatible threads |
| Process exposure | Temperature range, oils, cleaners, moisture, dust, and contact duration | Determines the required body and seal compatibility review |
| Air and flow demand | Air-quality requirement, supply condition, tube ID and length, duty cycle | Supports a whole-branch flow and maintenance assessment |
| Service access | Isolation point, release-ring clearance, inspection access, replacement route | Reduces avoidable disruption during planned maintenance |
Find leaks before they affect production
A compressed-air leak can increase compressor demand and may change local actuator behavior; its effect depends on leak size, storage, regulation, line capacity, and the motion being controlled. Treat it as an engineering finding, not proof that a fitting alone is defective. Inspect tube cuts, insertion depth, damaged tube, pull load, thread seal method, vibration, and port condition before replacing components.
ISO 4414 sets general pneumatic-system safety requirements; it is not blanket certification for an individual fitting. In the United States, OSHA 29 CFR 1910.242(b) limits compressed air used for cleaning to 30 psi or less with effective chip guarding and personal protective equipment. That rule does not establish 自動化-circuit pressure. Requirements depend on destination market, intended use, equipment risk assessment, and finished-system claims.
Set up a simple inspection routine
- Map each air branch from preparation unit to end device, including tube sizes, thread forms, reducers, valves, and moving sections.
- Specify normal and maximum pressure, temperature, media, air-quality requirement, process exposure, and required documentation for the exact part.
- Select the configuration that preserves routing clearance and avoids tight bends or unnecessary adapters. For common tube-end designs, compare the operating requirements with one-touch fitting selection guidance.
- Cut tubing squarely, follow the manufacturer’s insertion and sealing instructions, then test the completed branch under representative controlled conditions.
- Maintain an approved pairing list for tube and fitting part numbers; inspect moving routes, fittings near heat sources, and connections exposed to cleaning chemicals on the site’s planned schedule.
Unit price is only one buying input. Extra adapters, poor access, or missing technical data can add engineering and maintenance work. OULU can support an application-led inquiry for pneumatic straight fittings and related connections when a drawing, tube specification, and service conditions are available.
Match the fitting to the machine movement
Plastic-processing equipment often combines fixed manifolds, moving robot axes, hot tooling and frequent changeovers. A fitting suitable for a fixed control panel may fail when the tube is repeatedly bent at a robot wrist. Record the movement, bend radius, temperature, oil or cleaning exposure, point-of-use flow and service access before selecting the connector.
| Machine area | Main selection concern | Check before release |
|---|---|---|
| Fixed manifold | Thread, seal and port alignment | Gauge the thread and torque to the drawing |
| Robot or actuator | Tube movement and side load | Leave bend support and inspect for rubbing |
| Hot or chemical area | Temperature and media compatibility | Confirm the exact seal and tubing limits |
| Frequent changeover | Release access and spare consistency | Use one approved fitting family where possible |
Use the pneumatic fitting selection guide for material and thread checks, then compare one-touch limits before standardizing the machine spares.
Related reading: air-hose fitting sourcing guide.
How do heat, chemicals and movement change a plastics-process fitting?
A plastics line can combine robotic motion, cleaning agents, warm tooling, oil or moisture and repeated cycles. The fitting, tube and seal must be assessed as one assembly: a material suitable for dry control air may need a different review when it sees a chemical cleaner, elevated temperature or constant flexing. ISO 8573-1 helps state the compressed-air purity requirement, but it does not certify a fitting material or elastomer for every process chemical.
At moving axes, support the first bend and keep the fitting out of the load path. At hot or contaminated locations, confirm the exact tube and cover material; SMC’s spatter-resistant tubing page illustrates why a construction and flame-resistance statement belongs to a specified series rather than every multilayer tube. Inspect recurring failures at the same bend or port, because replacing the fitting without changing the route can repeat the downtime.
| Process condition | 確認 | Maintenance signal |
|---|---|---|
| Robot movement | Bend support, cycle and strain | Leak appears only during motion |
| Heat or spatter | Tube/cover material and distance | Hardening, discoloration or surface damage |
| Cleaning chemicals | Body, seal and tube compatibility | Swelling, cracking or recurring seepage |
| Wet or dirty air | Filtration and drain condition | Contamination at seal or valve |
よくある質問
Why are pneumatic fittings used in plastic manufacturing?
They connect compressed-air tubing to valves, actuators, grippers, manifolds, and process auxiliaries, while enabling branches and direction changes. Their suitability depends on the whole circuit-particularly interfaces, flow demand, movement, and exposure. Document those conditions before selecting a geometry.
What pneumatic fitting materials suit plastic processing plants?
Engineered polymers, brass, and stainless steel can each be considered, but no body material is universally suitable. Evaluate the fitting body, seal, and tube against heat, oils, cleaners, moisture, and the actual compressed-air condition. Obtain compatibility guidance for the exact model and exposure.
How do I choose fittings for robotic pick-and-place lines?
Start with motion range, tube bend radius, routing clearance, actuator flow need, and the port interface. Position elbows and supports to limit side load, and ensure release rings remain accessible. Run the intended motion cycle and inspect the connection before standardizing it.
Can compressed air leaks affect plastics production?
They can add air demand and, depending on circuit capacity and timing, contribute to inconsistent local pneumatic behavior. Diagnose the entire branch, including tubing, port sealing, and moving loads, rather than attributing every symptom to a fitting. A controlled leak and function check provides evidence for the repair decision.
How do heat and chemicals affect pneumatic tubing and fittings?
They may change material behavior or seal performance, and the result depends on chemical identity, concentration, temperature, duration, and mechanical stress. Cleaner overspray and radiant heat deserve the same review as the conveyed medium. Use current supplier documentation for the assembled tube, seal, and fitting combination.
What maintenance checks reduce unplanned downtime?
Use planned checks for damage, tube cuts, insertion depth, side load, vibration, abrasion, leakage, and restricted access. Review moving routes through a representative cycle and keep approved replacements tied to documented tube and fitting pairings. Escalate recurring findings to the equipment owner for a root-cause review.
Related reading: Oulu Connector company information.
参考文献
- ISO 4414:2010 – pneumatic system safety.
- ISO 6358-1 – flow-rate characteristics.
- ISO 8573-1 – compressed-air contaminants.
- SMC series-specific spatter-resistant tubing.
Summary
In plastics manufacturing, a fitting must match the air circuit and the machine environment. Confirm tube OD, thread, seal, pressure, temperature and air quality, then add movement, cleaning chemistry, heat and access to the review. ISO 4414 and ISO 8573-1 frame system safety and compressed-air quality; they do not certify a generic fitting for every process. Support moving tubing, inspect the first bend and investigate recurring damage at the route as well as the fitting. Record the process condition when a part is replaced so repeated failures can be compared across shifts. Oulu’s pneumatic parts range can be evaluated with the machine drawing, cycle conditions and maintenance record rather than a catalogue shape alone.